01
No mould required
Batch and short-run production without a die. The drawing is the tooling, so a design change is a file change, not a new mould and a new lead time. A prototype and a production run come off the same setup.
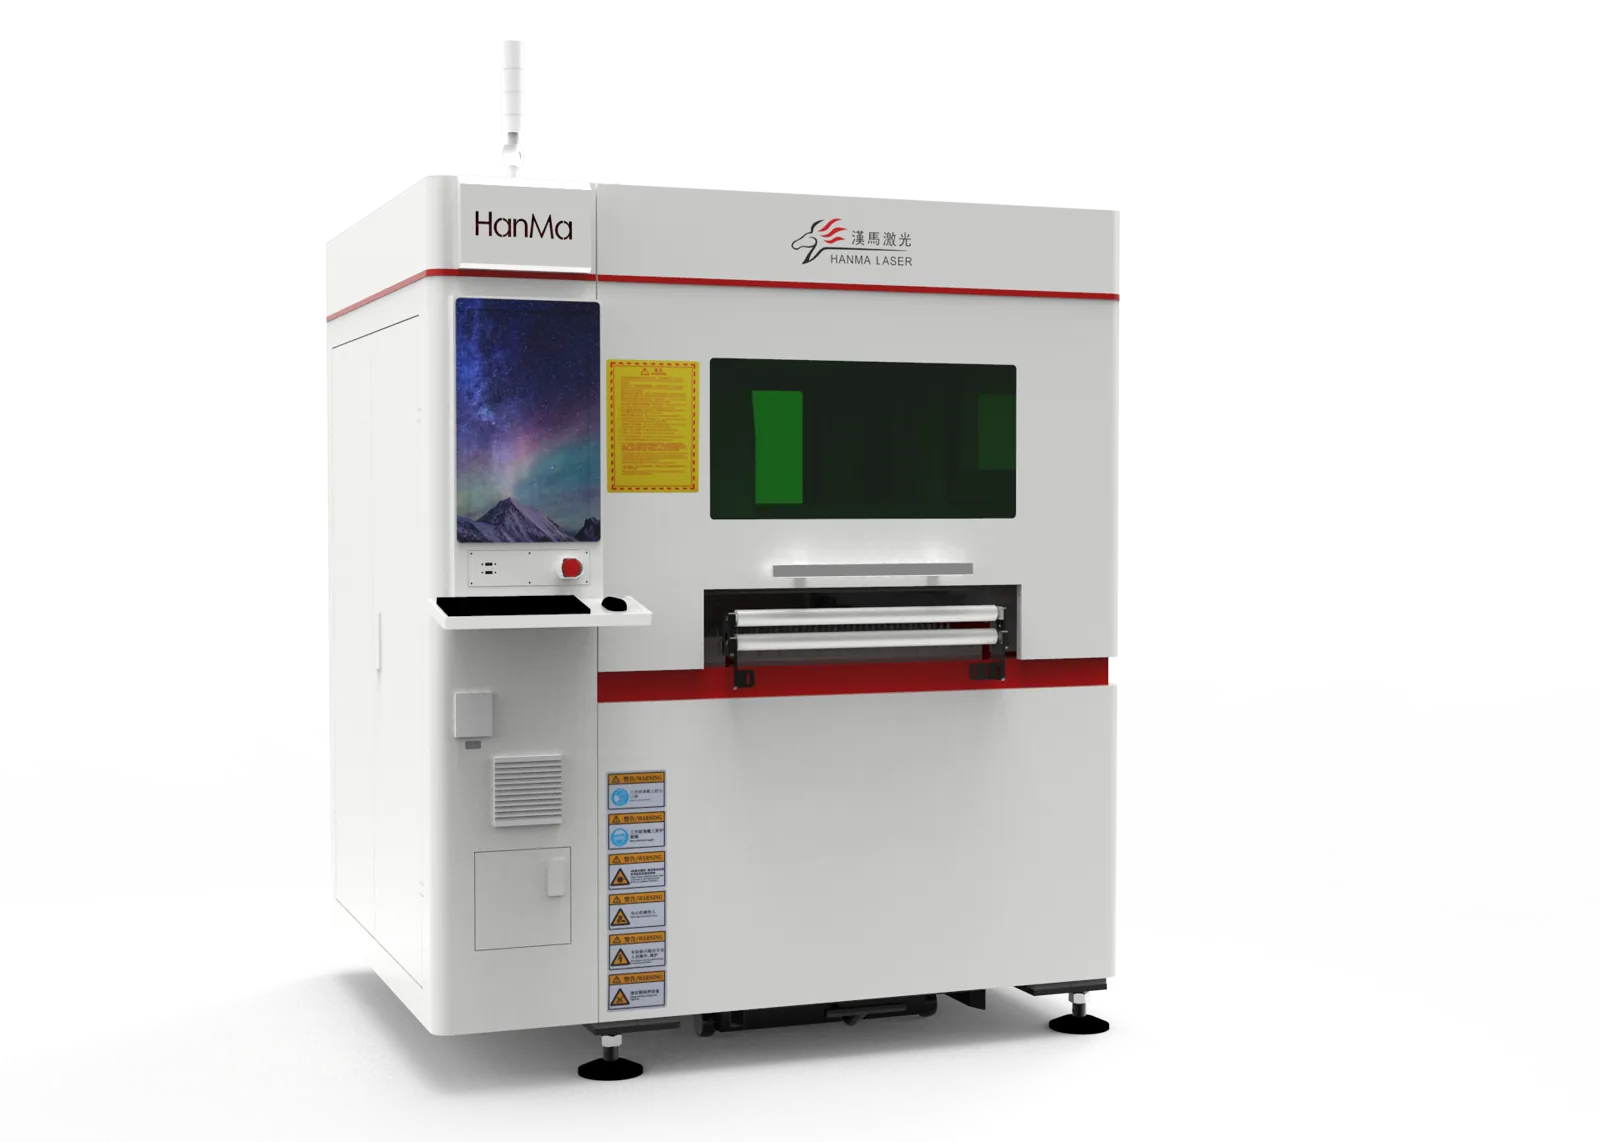
Adspark supplies and supports the HANMA HM-GX precision fibre laser cutting range across South East Asia. No mould, no tooling lead time, and ±0.02 mm on the parts that decide whether the assembly works, delivered with engineers who stay on your floor long after installation.
Precision cutting & drilling · South East Asia
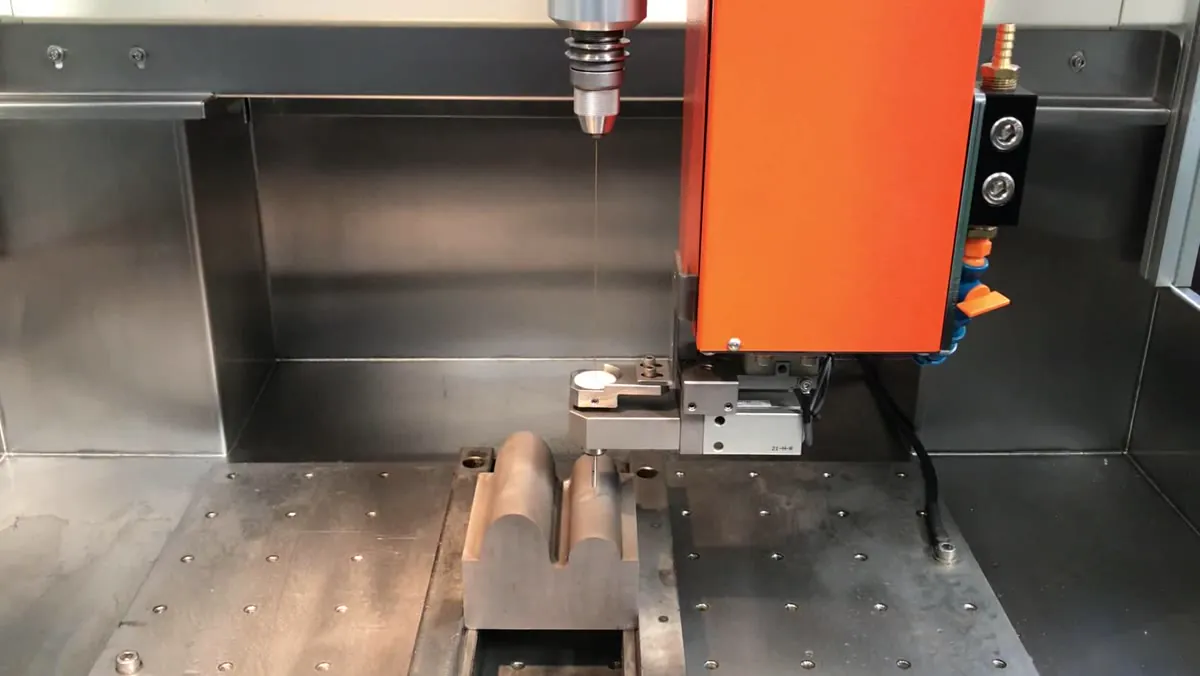
Adspark runs a deliberately tight range: the HM-GX fibre cells that cut metal to a fine tolerance without a mould, and the Super Drill that sinks small, deep holes by EDM where a drill cannot go. We chose each machine, we run them every day, and we support them from five offices, so what lands on your floor is a machine we already know inside out.
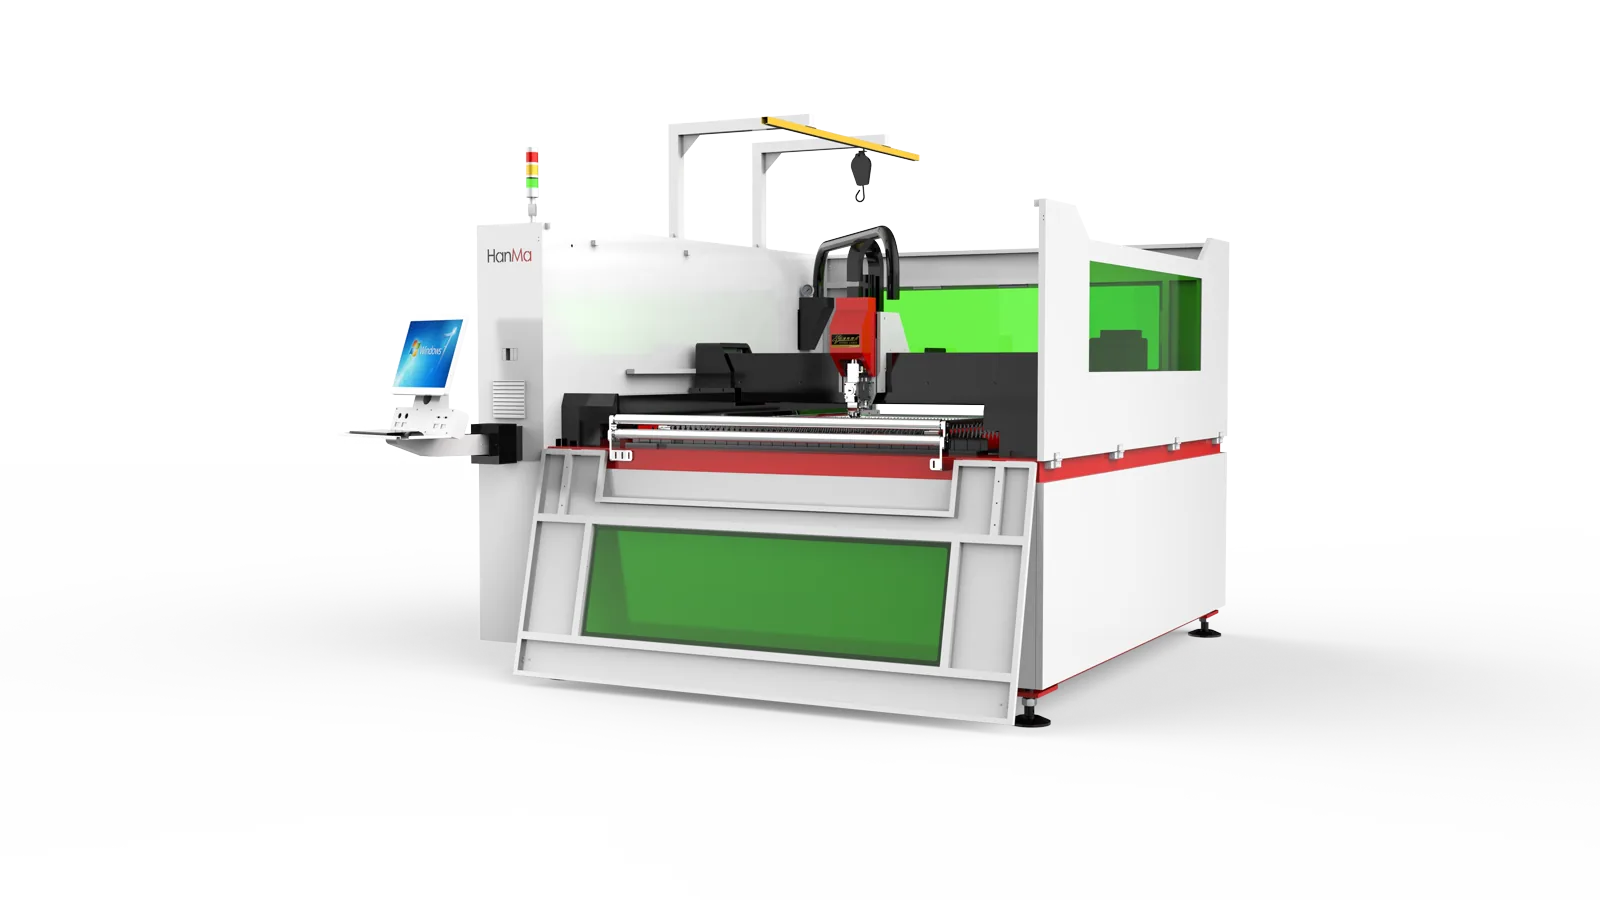
One team, two processes. The HM-GX1313 and HM-GX6060 cut metal to ±0.02 mm with no mould; the Super Drill sinks small, deep holes by EDM into metal too hard for a drill. We run all three on our own floor before they land on yours.
Manufactured by HANMA Laser · 汉马激光
Certified precision, in a certified supply chain.
Exported to United States, Germany, United Kingdom, Canada, the HM-GX line is proven in the world's most demanding industrial markets.
No mould, a sealed fibre path and a precision-milled body, the reasons the HM-GX line cuts faster, cleaner and for longer than the alternatives it replaces.
Batch and short-run production without a die. The drawing is the tooling, so a design change is a file change, not a new mould and a new lead time. A prototype and a production run come off the same setup.
A 1.06 μm beam, one tenth the CO₂ wavelength, is absorbed better by metal. That means clean, fast cuts in carbon steel, stainless and aluminium, and in reflective non-ferrous like brass and copper that other processes struggle with.
Automatic loading and unloading keeps the cell fed for continuous, automated coordination rather than one blank at a time. It holds pace with the production line around it instead of gating it.
Every machine is milled and stress-relieved so it holds its geometry at speed. That is what keeps the cut smooth without shake, so the last part of a long run measures like the first.
Roughly three square metres of floor, with a vertical sliding door and a large front opening. It fits where a press line never could, and it is commissioned and running in a day or two.
The laser travels a sealed, constant optical path straight to the head. Simple mechanics and a semiconductor, redundant laser design mean it is rated for 24-hour continuous, industrial duty.
A walkaround of the HANMA cell in the workshop, with the cutting head tracking a motor-lamination nest on the CNC screen, running on real material before it is ever crated. Nothing here is a render. What you see is the machine that arrives.
Professionally calibrated cutting speed
Compact machine footprint
After-sales response commitment
Offices across South East Asia
We deliver a complete cutting solution: the machine, the process, the assist-gas setup and the people who know how to run it arrive together, not as a box on a pallet. You are buying the outcome, not just the equipment.
Bring us the part that will not cut cleanly. We run your drawing and your material on the machine, and send back the sample and the exact parameters that produced it, so you decide with the part in your hand.
Five offices across South East Asia mean the engineer who answers the call is close enough to be on your floor. Installation, commissioning and service stay within reach, not a continent away.
The HM-GX line is ISO 9001, CE and FDA certified and exported to the US, Germany, the UK and Canada. It is precision you can place in a certified, traceable supply chain with the paperwork to match.
Fine features and tight tolerances on small, high-value components where a burr means a reject.
Silicon-steel stator and rotor laminations for motors and EV drivetrains, cut without a die.
Aluminium-based sheets, heat-dissipation plates and cooling nets at repeatable accuracy.
Multi-cavity connector detail and fine-pitch mould parts with clean, vertical edges.
Small hardware, gears and fittings cut clean with no burr roll and no finishing pass.
Meshes, filters, apertures and micro-hole plates held to repeat accuracy across the run.
Send us the material, the tolerance and the part you cannot get cut. An engineer, not a form robot, will read it.